Single Stage Water Ring Vacuum Pumps
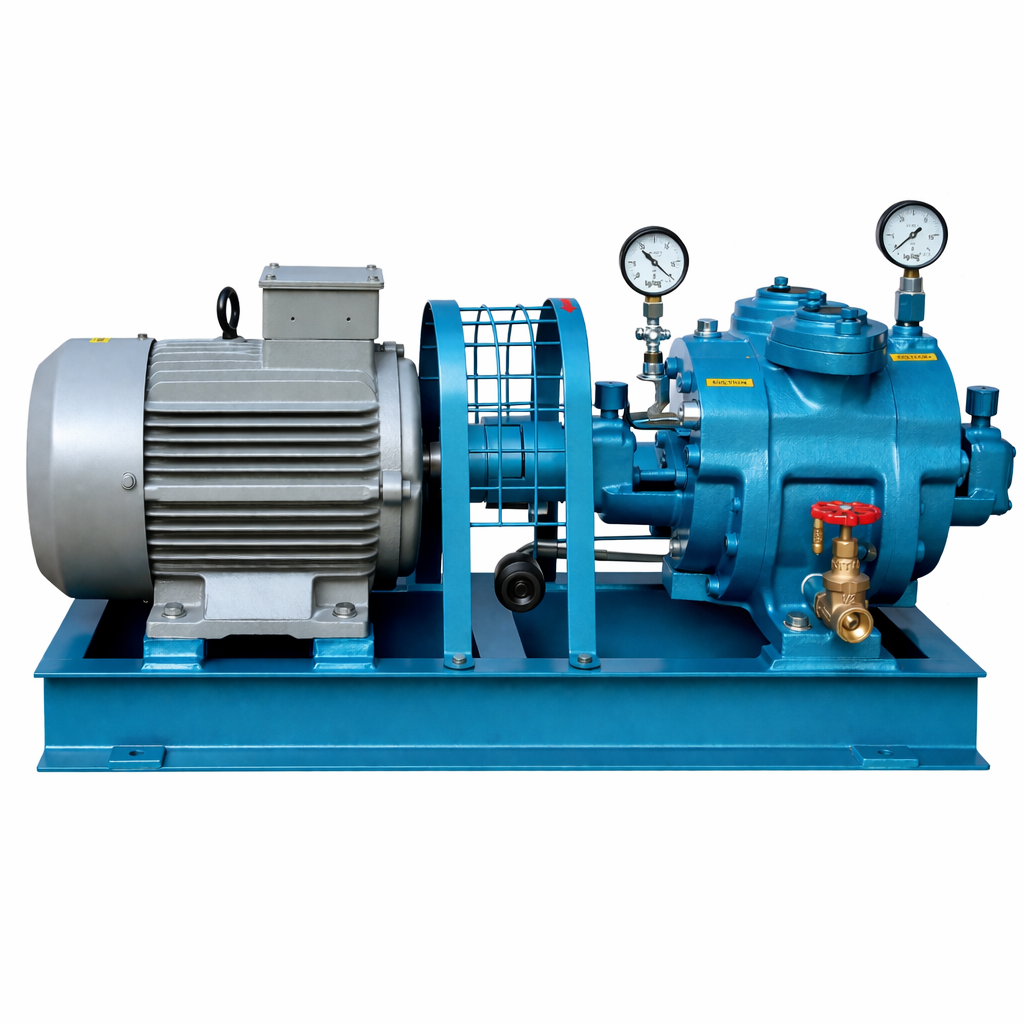
Product Overview
Single Stage Water Ring Vacuum Pumps are industrial vacuum solutions designed to handle wet, humid, and vapor-laden gases efficiently. Using water or a compatible liquid as the sealing medium, these pumps generate a stable vacuum while helping manage moisture and condensable vapors. They are suitable for industries that require dependable vacuum performance under challenging operating conditions. Richa Engineering manufactures vacuum pumps with a focus on reliable construction, consistent operation, and application-oriented engineering. With a vacuum range of up to 33 mbar, depending on operating conditions, these pumps are a practical choice for chemical processing, pharmaceutical, paper, food processing, power plants, and other industrial applications.
Key Features of Single Stage Water Ring Vacuum Pumps
Water Ring Technology
The pump uses water or a compatible liquid as the sealing medium, making it suitable for wet-gas and vapor-handling applications.
Effective Moisture & Vapor Handling
The liquid-ring operating principle allows the pump to handle gases containing moisture, vapors, and condensable components.
Smooth & Low-Noise Operation
The water ring provides smooth compression and helps minimize friction and vibration during operation.
Robust Construction
Available in Cast Iron and Stainless Steel construction options to support different industrial requirements.
Industrial Vacuum Performance
The pump can achieve a vacuum level of up to 33 mbar, depending on operating conditions, making it suitable for a broad range of moderate-vacuum industrial processes.
Single Stage Water Ring Vacuum Pump Specifications
Explore the key technical specifications of our Single Stage Water Ring Vacuum Pump, designed for reliable vacuum generation in demanding industrial applications.
| Parameter | Specification |
|---|---|
| Pump Type | Single Stage Water Ring Vacuum Pump |
| Vacuum Range | Up to 33 mbar, depending on conditions |
| Pumping Capacity | Wide range available |
| Construction | Cast Iron / Stainless Steel |
| Seal Liquid | Water or compatible fluids |
| Mounting | Horizontal |
| Operating Principle | Eccentric impeller with liquid ring |
| Application | Wet gases, vapors and industrial vacuum processes |
Note: Actual vacuum performance and pumping capacity may vary according to operating conditions, seal liquid temperature, gas composition and system configuration.
Benefits of Single Stage Water Ring Vacuum Pumps
Choosing the right liquid-ring vacuum pump can improve process reliability and simplify vacuum generation in demanding industrial environments. The water-sealed operating principle eliminates the need for oil as the primary sealing medium, which can be beneficial in processes where moisture and vapors are present.
The robust construction supports dependable industrial operation, while the smooth rotating mechanism helps maintain stable vacuum performance. These pumps are also suitable for continuous-duty applications where consistent suction is important. Their ability to handle wet gases and condensable vapors can reduce performance problems associated with moisture entering the vacuum system.
For industries seeking a practical and durable vacuum solution, a Single Stage Water Ring Vacuum Pump can provide a balance of reliable performance, straightforward operation, and application flexibility.
Applications of Single Stage Water Ring Vacuum Pumps
Single Stage Water Ring Vacuum Pumps are used across industries where vacuum generation involves wet gases, humidity, vapors, or condensable materials.
Chemical Processing
Chemical processes often generate vapors and moisture that conventional vacuum technologies may struggle to handle efficiently. Water ring pumps provide a suitable solution for these environments.
Pharmaceutical Industry
Vacuum is used in several pharmaceutical processes where controlled and reliable suction is required. Liquid-ring technology can be useful when moisture or vapor handling is involved.
Paper & Pulp Industry
Paper manufacturing processes frequently require vacuum for water removal and process handling. Water ring pumps can support reliable vacuum generation in these operations.
Food Processing
Food processing applications may require vacuum for evaporation, packaging, drying, or other process requirements where moisture handling is important.
Power Plants
Water ring vacuum pumps can be used in industrial utility and power-generation processes requiring dependable vacuum operation.
They are also applicable to other industrial processes where reliable vacuum generation and wet-gas handling are important.
How Does a Single Stage Water Ring Vacuum Pump Work?
The operating principle is based on the formation of a liquid ring inside the pump casing. An impeller is positioned eccentrically within a cylindrical casing that contains water or another compatible sealing liquid.
As the impeller rotates, centrifugal force pushes the liquid toward the casing wall, creating a rotating liquid ring. The eccentric position of the impeller causes the volume between the impeller blades and liquid ring to change continuously.
When these chambers increase in volume, gas is drawn into the pump through the inlet. As the chambers decrease in volume, the trapped gas is compressed and discharged through the outlet. Throughout the process, the liquid provides sealing and cooling, allowing the pump to operate effectively when handling wet gases and vapors.
Why Choose Richa Engineering for Water Ring Vacuum Pumps?
Richa Engineering is an experienced vacuum equipment manufacturer based in Ahmedabad, Gujarat, with 25+ years of industrial experience. The company manufactures vacuum pumps, roots blowers, vacuum boosters, and precision-engineered spare parts for industrial and laboratory applications. Its product range includes liquid ring pumps, water ring pumps, and two-stage pumps.
The company focuses on engineering, material selection, manufacturing processes, and quality checks to deliver reliable vacuum solutions. Its manufacturing approach is designed around customer requirements, product durability, and consistent industrial performance. Technical support and application-oriented selection can also help customers choose an appropriate vacuum pump for their process.
Get the Right Single Stage Water Ring Vacuum Pump for Your Application
Looking for a reliable Single Stage Water Ring Vacuum Pump for wet gases, vapors, or industrial vacuum applications? Richa Engineering can help you select a suitable pump based on your required vacuum level, capacity, construction material, and process conditions. Contact Richa Engineering today to request a quotation and discuss your vacuum pump requirements.
Get in Touch
Looking for a dependable solution for wet and vapor-heavy vacuum applications?
Contact us today to get the best Single Stage Water Ring Vacuum Pump tailored to your needs..